Why this question comes up: the physics
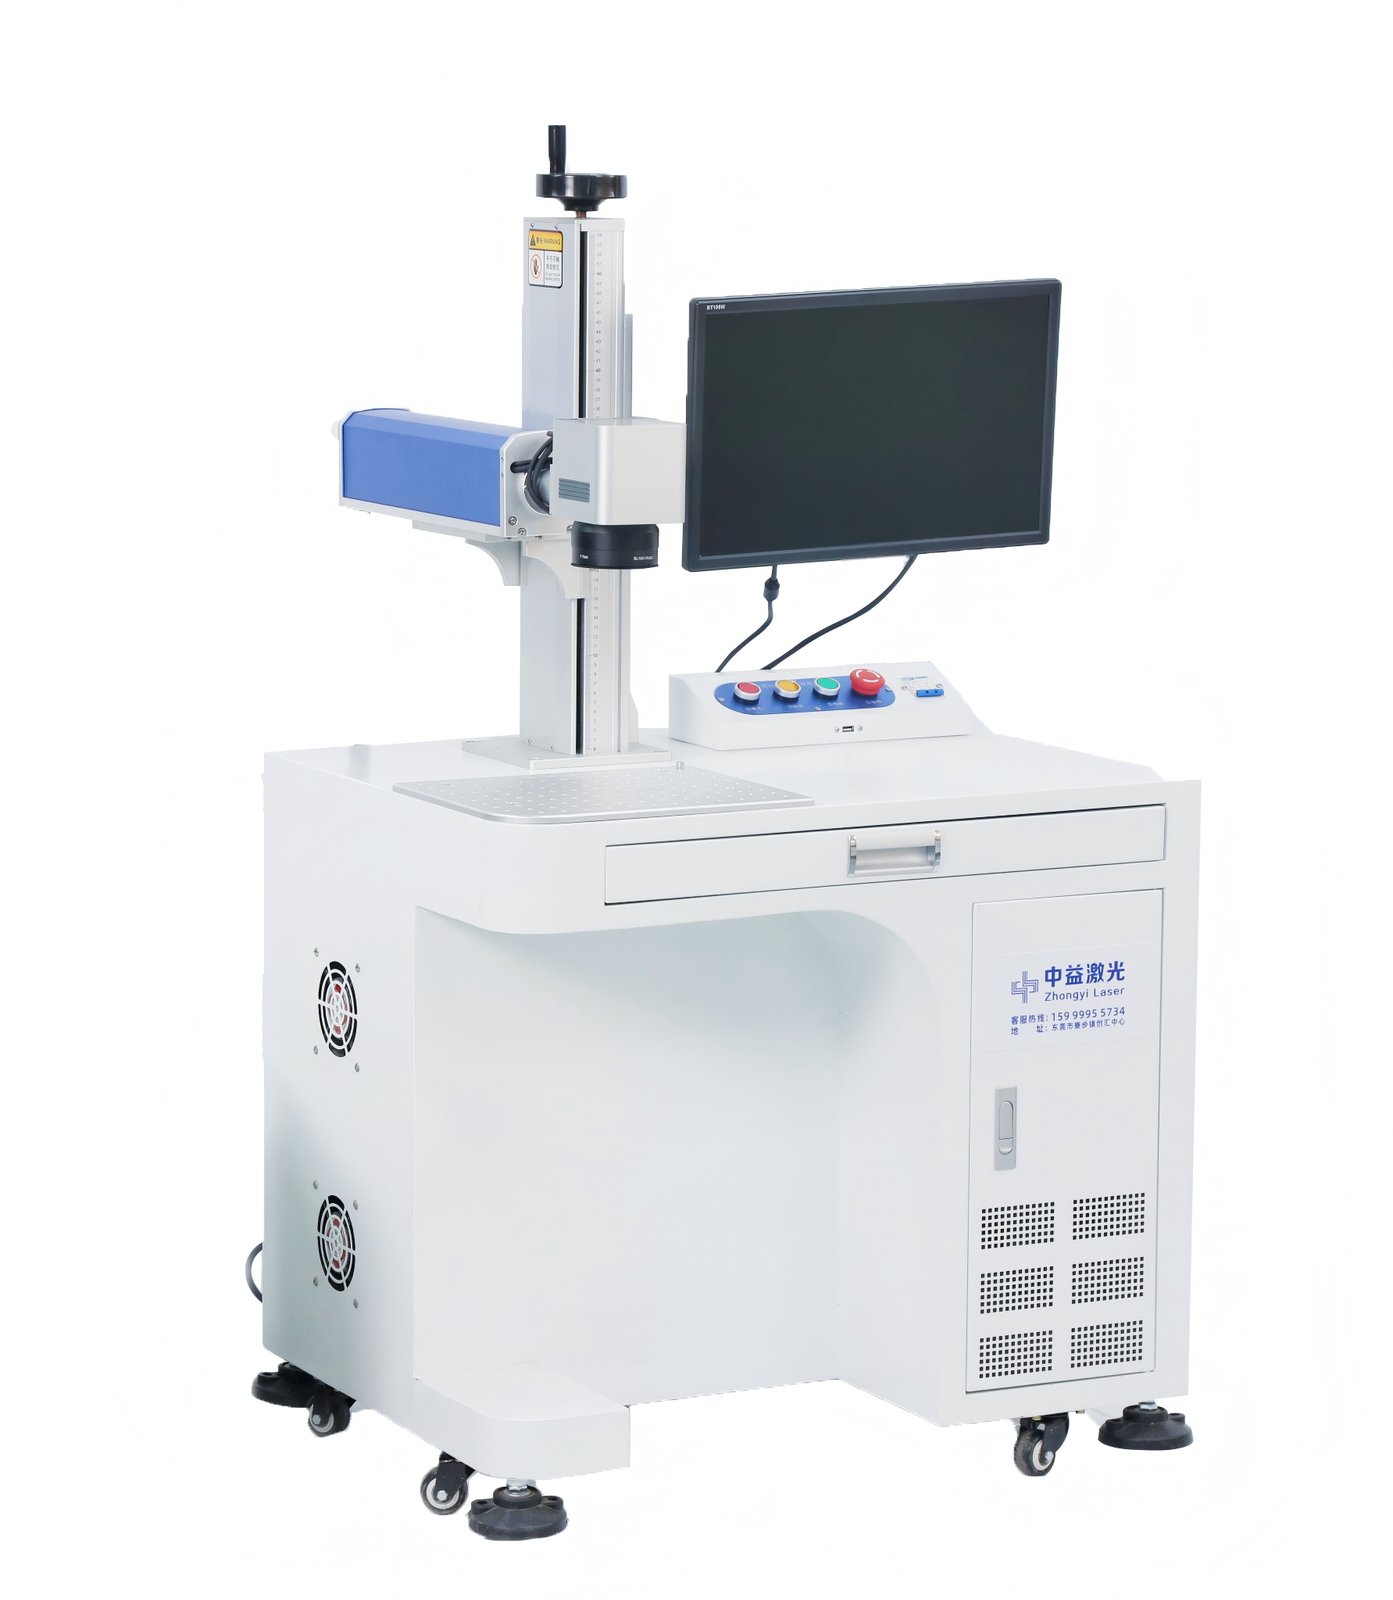
A fiber laser marker runs at 1064 nm, which metals absorb efficiently. Heat melts, oxidises or vaporises the surface, and because the mark is integral to the base metal it cannot peel. We build fiber units from 20 to 200 W with JCZ EzCad control software, supporting deep engraving, black marking and colour oxidation on stainless steel, where a MOPA source controls oxide film thickness through pulse width and frequency.
The answer and the process detail
A single pass typically removes tens of micrometres to around 0.1 mm; depth is built up by layering. Each layer's slag must be blown clear or the next layer becomes far less efficient. Depth scales roughly linearly with time, so anything beyond 0.5 mm needs a cycle-time check. For metal deep engraving start at 50 W and use 100 W or more in production. Send the steel grade and target depth and the engineer will quote layers and estimated run time.
How to set it up and verify it
Depth is governed by single-pulse energy and pass count, not wattage alone: lowering the frequency raises pulse energy and deepens each pass, while higher speed and wider hatch spacing make it shallower. Deep engraving normally runs low frequency, slow speed and multiple layers, with time between layers for slag to clear and heat to dissipate, otherwise the next layer drops sharply in efficiency. Always run a step test before production and archive one standard sample per day so drift is visible.
Selection and delivery
For black marking and shallow identification 20 W is enough and costs less; deep engraving, high volumes or fast-conducting metals such as copper and aluminium start at 50 W and run 100 W and above in production. Volume orders can add a rotary axis for round parts, array fixtures for throughput, and automatic loading to feed the line. Full power range, materials and buyer Q&A are on the Fiber Laser Marking Machine page.
Procurement Q&A
Open Mo–Su 08:00–23:00 (GMT+8) with English support. Reach us at +86 159 9995 5734, WhatsApp +86 190 9874 6815 or [email protected]. Machines are packed to export standards.
We have 3+ engineers, 7+ authorised patents and 5000+ units shipped. Standard parts like laser source and galvo are stocked long-term for predictable replenishment.
Price depends on the model (UV / fiber / CO₂), power, laser-source brand (Raycus / JPT / IPG) and configuration (galvo, field lens, control software). Zhongyi Laser lists the exact laser-source and galvo models on the quote and in the contract, so the configuration is verifiable and easy to reorder or replace later.
Standard machines ship in 7 days; rush orders in 3–5 days; custom non-standard builds in 15–30 days. Before production we confirm drawings, process and sample results to avoid rework.
18-month warranty on the machine. Core parts like the laser source and galvo are replaceable standard parts with long-term supply, so repairs and swaps are documented.
Yes. Send a sample and we return a real test video within 24 hours and ship the part back. Key models get a 48-hour aging test, so you see the actual result on your own workpiece before deciding.
A single pass typically removes tens of micrometres to around 0.1 mm; depth is built up by layering. Each layer's slag must be blown clear or the next layer becomes far less efficient. Depth scales roughly linearly with time, so anything beyond 0.5 mm needs a cycle-time check. For metal deep engraving start at 50 W and use 100 W or more in production. Send the steel grade and target depth and the engineer will quote layers and estimated run time.
Yes. Fiber at 1064 nm re-melts and oxidises the surface of gold, silver and copper, so the mark is integral to the base metal - it is not a coating that can peel. Only subsequent mechanical polishing or chemical treatment will remove it. Where a permanent traceable mark is required, deep engraving is safer than shallow. Our fiber range runs 20 to 200 W and can be fitted with a rotary axis for rings and bangles.
Two questions: what effect, and what throughput. For black marking and shallow identification, 20 W is enough and costs less. For deep engraving, high volumes or fast-conducting metals such as copper and aluminium, 50 W and above earns its keep. Colour marking on stainless needs a MOPA source, where pulse width and frequency control oxide film thickness. Give us the alloy grade, required effect and cycle time per part and the engineer will recommend a power.