Why this question comes up: the physics
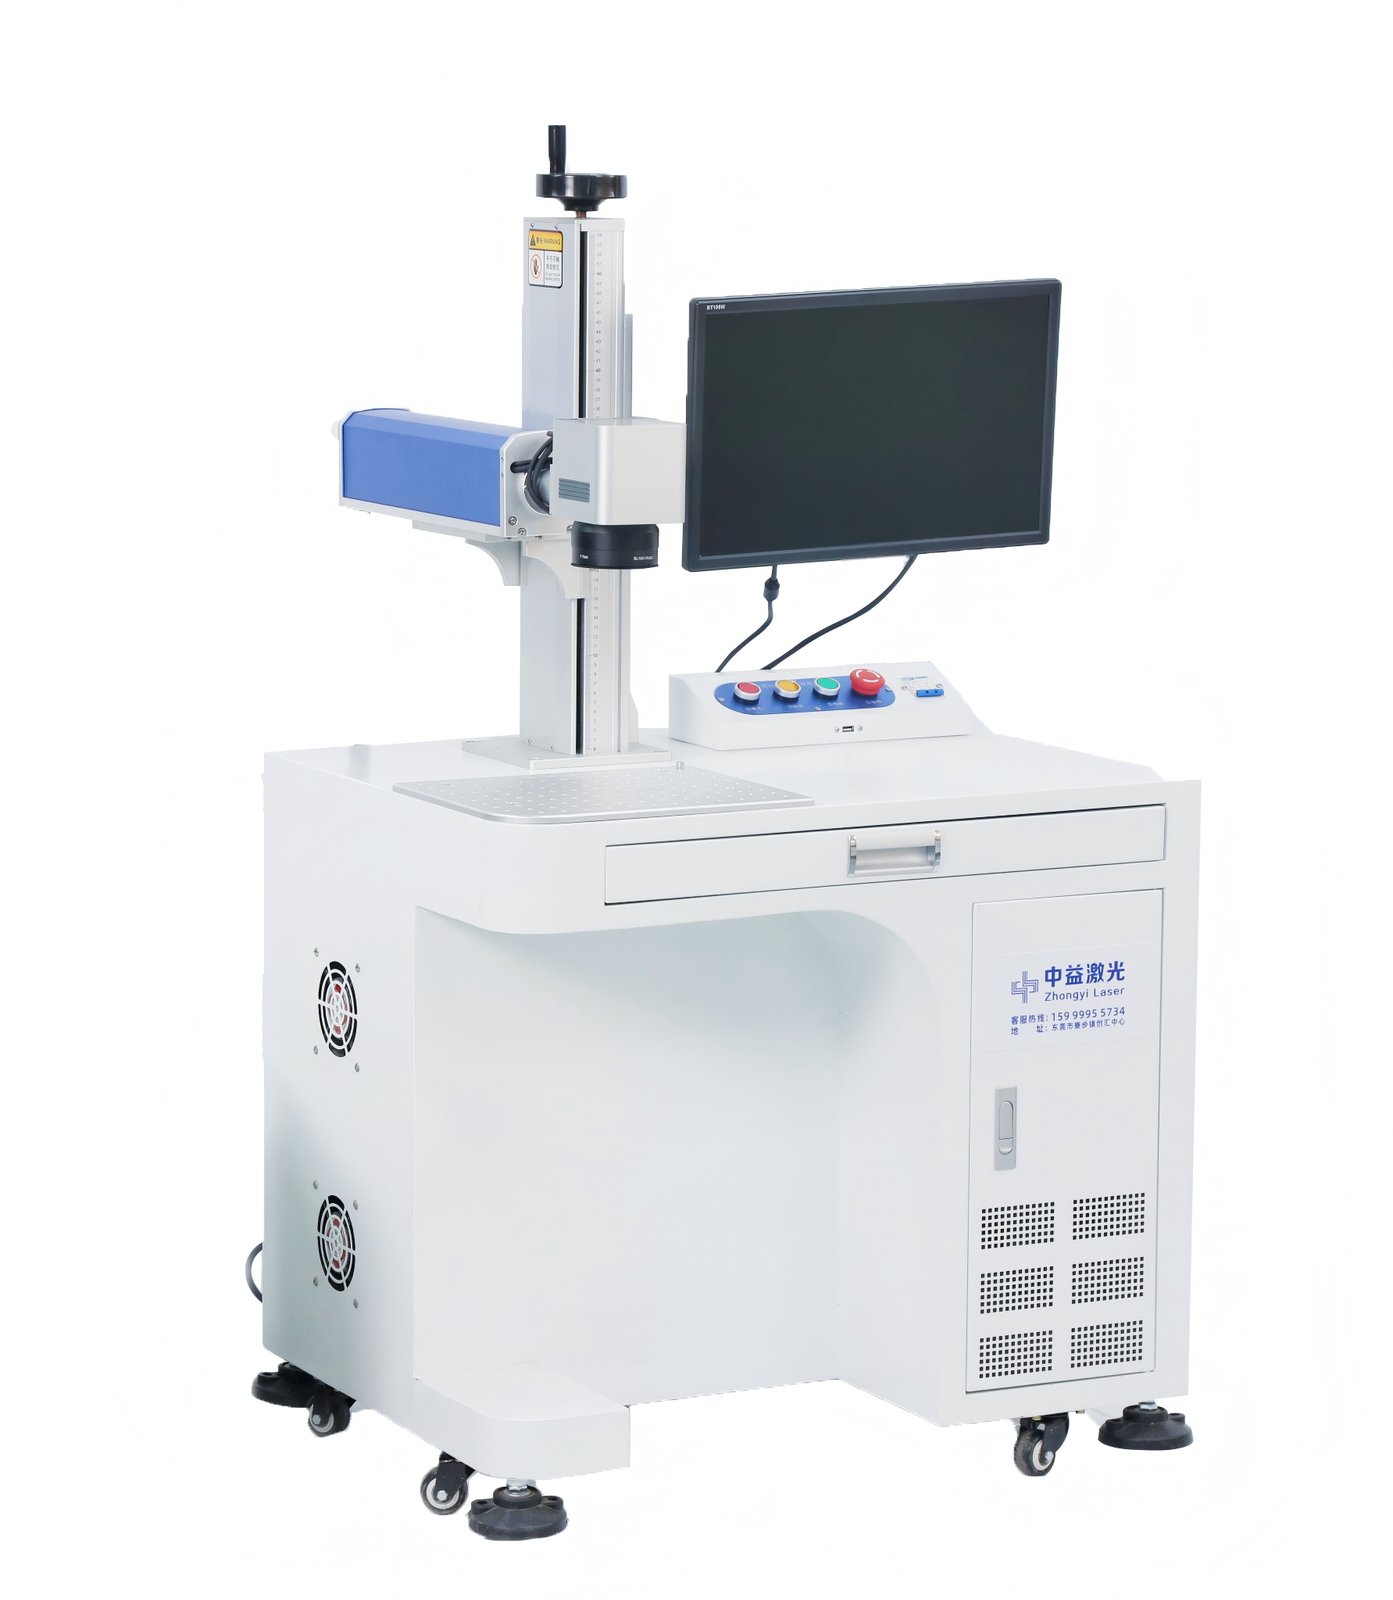
A fiber laser marker runs at 1064 nm, which metals absorb efficiently. Heat melts, oxidises or vaporises the surface, and because the mark is integral to the base metal it cannot peel. We build fiber units from 20 to 200 W with JCZ EzCad control software, supporting deep engraving, black marking and colour oxidation on stainless steel, where a MOPA source controls oxide film thickness through pulse width and frequency.
The answer and the process detail
Yes. The rotary axis converts angular displacement into linear travel, and the software's cylindrical unwrap function lays the artwork continuously around rings, pen barrels or tubes. The critical setting is pulses per revolution matched to workpiece diameter - get it wrong and the pattern stretches or the seam misaligns. We supply rotary fixtures; tell us the actual diameter when you send samples and we will verify seam alignment in the marking video.
How to set it up and verify it
Depth is governed by single-pulse energy and pass count, not wattage alone: lowering the frequency raises pulse energy and deepens each pass, while higher speed and wider hatch spacing make it shallower. Deep engraving normally runs low frequency, slow speed and multiple layers, with time between layers for slag to clear and heat to dissipate, otherwise the next layer drops sharply in efficiency. Always run a step test before production and archive one standard sample per day so drift is visible.
Selection and delivery
For black marking and shallow identification 20 W is enough and costs less; deep engraving, high volumes or fast-conducting metals such as copper and aluminium start at 50 W and run 100 W and above in production. Volume orders can add a rotary axis for round parts, array fixtures for throughput, and automatic loading to feed the line. Full power range, materials and buyer Q&A are on the Fiber Laser Marking Machine page.
Procurement Q&A
Yes. Send a sample and we return a real test video within 24 hours and ship the part back. Key models get a 48-hour aging test, so you see the actual result on your own workpiece before deciding.
Open Mo–Su 08:00–23:00 (GMT+8) with English support. Reach us at +86 159 9995 5734, WhatsApp +86 190 9874 6815 or Laurie@laserdg.com. Machines are packed to export standards.
We have 3+ engineers, 7+ authorised patents and 5000+ units shipped. Standard parts like laser source and galvo are stocked long-term for predictable replenishment.
Price depends on the model (UV / fiber / CO₂), power, laser-source brand (Raycus / JPT / IPG) and configuration (galvo, field lens, control software). Zhongyi Laser lists the exact laser-source and galvo models on the quote and in the contract, so the configuration is verifiable and easy to reorder or replace later.
Standard machines ship in 7 days; rush orders in 3–5 days; custom non-standard builds in 15–30 days. Before production we confirm drawings, process and sample results to avoid rework.
18-month warranty on the machine. Core parts like the laser source and galvo are replaceable standard parts with long-term supply, so repairs and swaps are documented.
Yes. The rotary axis converts angular displacement into linear travel, and the software's cylindrical unwrap function lays the artwork continuously around rings, pen barrels or tubes. The critical setting is pulses per revolution matched to workpiece diameter - get it wrong and the pattern stretches or the seam misaligns. We supply rotary fixtures; tell us the actual diameter when you send samples and we will verify seam alignment in the marking video.
Yes, this is one of fiber's strongest applications. Anodised layers absorb 1064 nm, and the surface is removed or modified to black against the silver base - a strong contrast that is integral to the part and cannot peel. Use moderate power with relatively high speed so you do not cut through to bright metal. A MOPA source gives finer greyscale through pulse width control. Send a sample and we will return a comparison.
Depth is governed by single-pulse energy and pass count, not by wattage alone. At a given power, lowering the frequency raises pulse energy and deepens each pass; raising scan speed or widening hatch spacing makes it shallower. Deep engraving normally runs low frequency, slow speed, multiple layers, with time between layers for debris to clear. 20 W suits shallow black marking; 50 W and above is where production deep engraving starts. We build fiber units from 20 to 200 W - give us the alloy and target depth and we will return a parameter sheet.