Why this question comes up: the physics
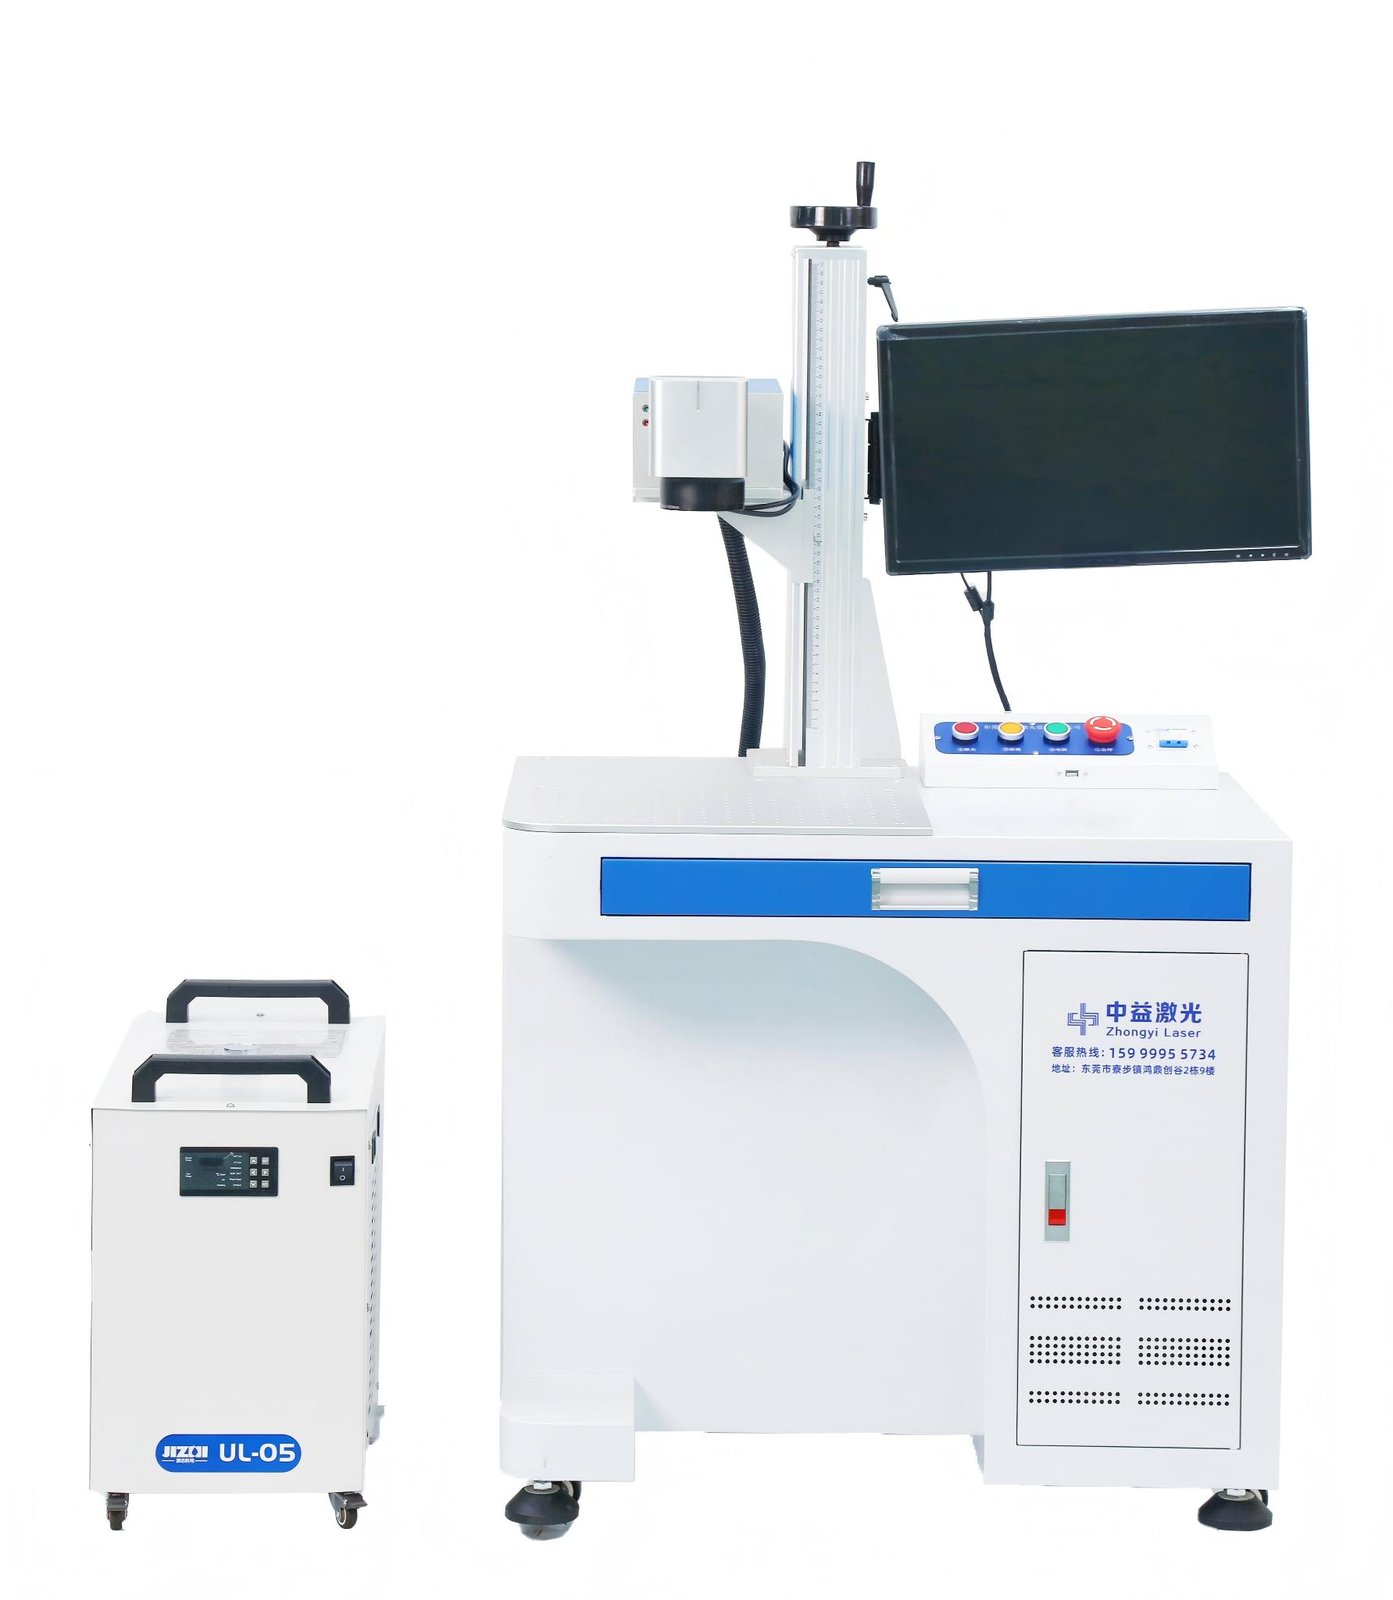
A UV laser marker works at 355 nm and is a cold process: photon energy breaks molecular bonds directly, stripping or modifying the surface photochemically with a minimal heat-affected zone, so heat-sensitive parts do not yellow, melt at the edges or stress-crack. Our UV platform focuses to 15 micrometres with plus or minus 0.02 mm repeatability, 110, 175 and 300 mm square fields, and a constant-temperature chiller locking the source temperature.
The answer and the process detail
Yes, this is a classic UV advantage. The coating and the substrate absorb 355 nm differently, and UV pulse energy is finely controllable with little heat spread, so the plated layer can be removed with minimal effect on the base. Parameters are the whole game: too much power breaks through to the substrate, too little leaves residue. Sweep upwards from low power until the coating clears and the substrate is untouched, then lock the file. Sampling is the fastest route.
How to set it up and verify it
Three knobs set the process: power, repetition rate and scan speed, which together determine energy density per unit area. Start low and map a parameter window - sweep power and frequency at a fixed speed, find the cell where contrast is acceptable and the edge is not carbonised, then lock it into a process file with permissions. Remember that cold does not mean heat-free: too much power, too low a frequency or too many passes still accumulate heat, and thin stock will still perforate or curl.
Selection and delivery
3 W and 5 W suit thin materials and very shallow marking, 10 and 15 W suit large filled areas and poorly absorbing materials, and 20 W is built to order. The deciding factor is not precision, which is essentially identical at the same spot size, but cycle time: divide daily output by available hours and work back to the power you need. Still unsure, send samples - we mark them free at our Dongguan factory and return both the parts and a marking video within 24 hours. Full specifications, materials and buyer Q&A are on the UV Laser Marking Machine page.
Procurement Q&A
Yes. Send a sample and we return a real test video within 24 hours and ship the part back. Key models get a 48-hour aging test, so you see the actual result on your own workpiece before deciding.
Open Mo–Su 08:00–23:00 (GMT+8) with English support. Reach us at +86 159 9995 5734, WhatsApp +86 190 9874 6815 or [email protected]. Machines are packed to export standards.
We have 3+ engineers, 7+ authorised patents and 5000+ units shipped. Standard parts like laser source and galvo are stocked long-term for predictable replenishment.
Price depends on the model (UV / fiber / CO₂), power, laser-source brand (Raycus / JPT / IPG) and configuration (galvo, field lens, control software). Zhongyi Laser lists the exact laser-source and galvo models on the quote and in the contract, so the configuration is verifiable and easy to reorder or replace later.
Standard machines ship in 7 days; rush orders in 3–5 days; custom non-standard builds in 15–30 days. Before production we confirm drawings, process and sample results to avoid rework.
18-month warranty on the machine. Core parts like the laser source and galvo are replaceable standard parts with long-term supply, so repairs and swaps are documented.
Yes, this is a classic UV advantage. The coating and the substrate absorb 355 nm differently, and UV pulse energy is finely controllable with little heat spread, so the plated layer can be removed with minimal effect on the base. Parameters are the whole game: too much power breaks through to the substrate, too little leaves residue. Sweep upwards from low power until the coating clears and the substrate is untouched, then lock the file. Sampling is the fastest route.
Yes. Repetition rate is one of the core adjustable parameters and, together with power and speed, sets pulse energy and overlap. High frequency suits fine, low-heat-input materials; low frequency gives higher pulse energy for poorly absorbing ones. MOPA sources allow independent pulse width control for even finer tuning. Frequency is adjustable across our UV range and parameter files can be saved per material.
Ceramic absorbs 355 nm well, so high contrast is easy, but over-burning yellows the surface. Start at low power to find the point where colour just appears, then fine-tune speed and frequency for uniformity, keeping hatch spacing tight to avoid banding. Ceramic conducts heat poorly, so excessive overlap causes local heat build-up. Keep separate files per material grade - alumina and aluminium nitride have noticeably different thresholds.