Why this question comes up: the physics
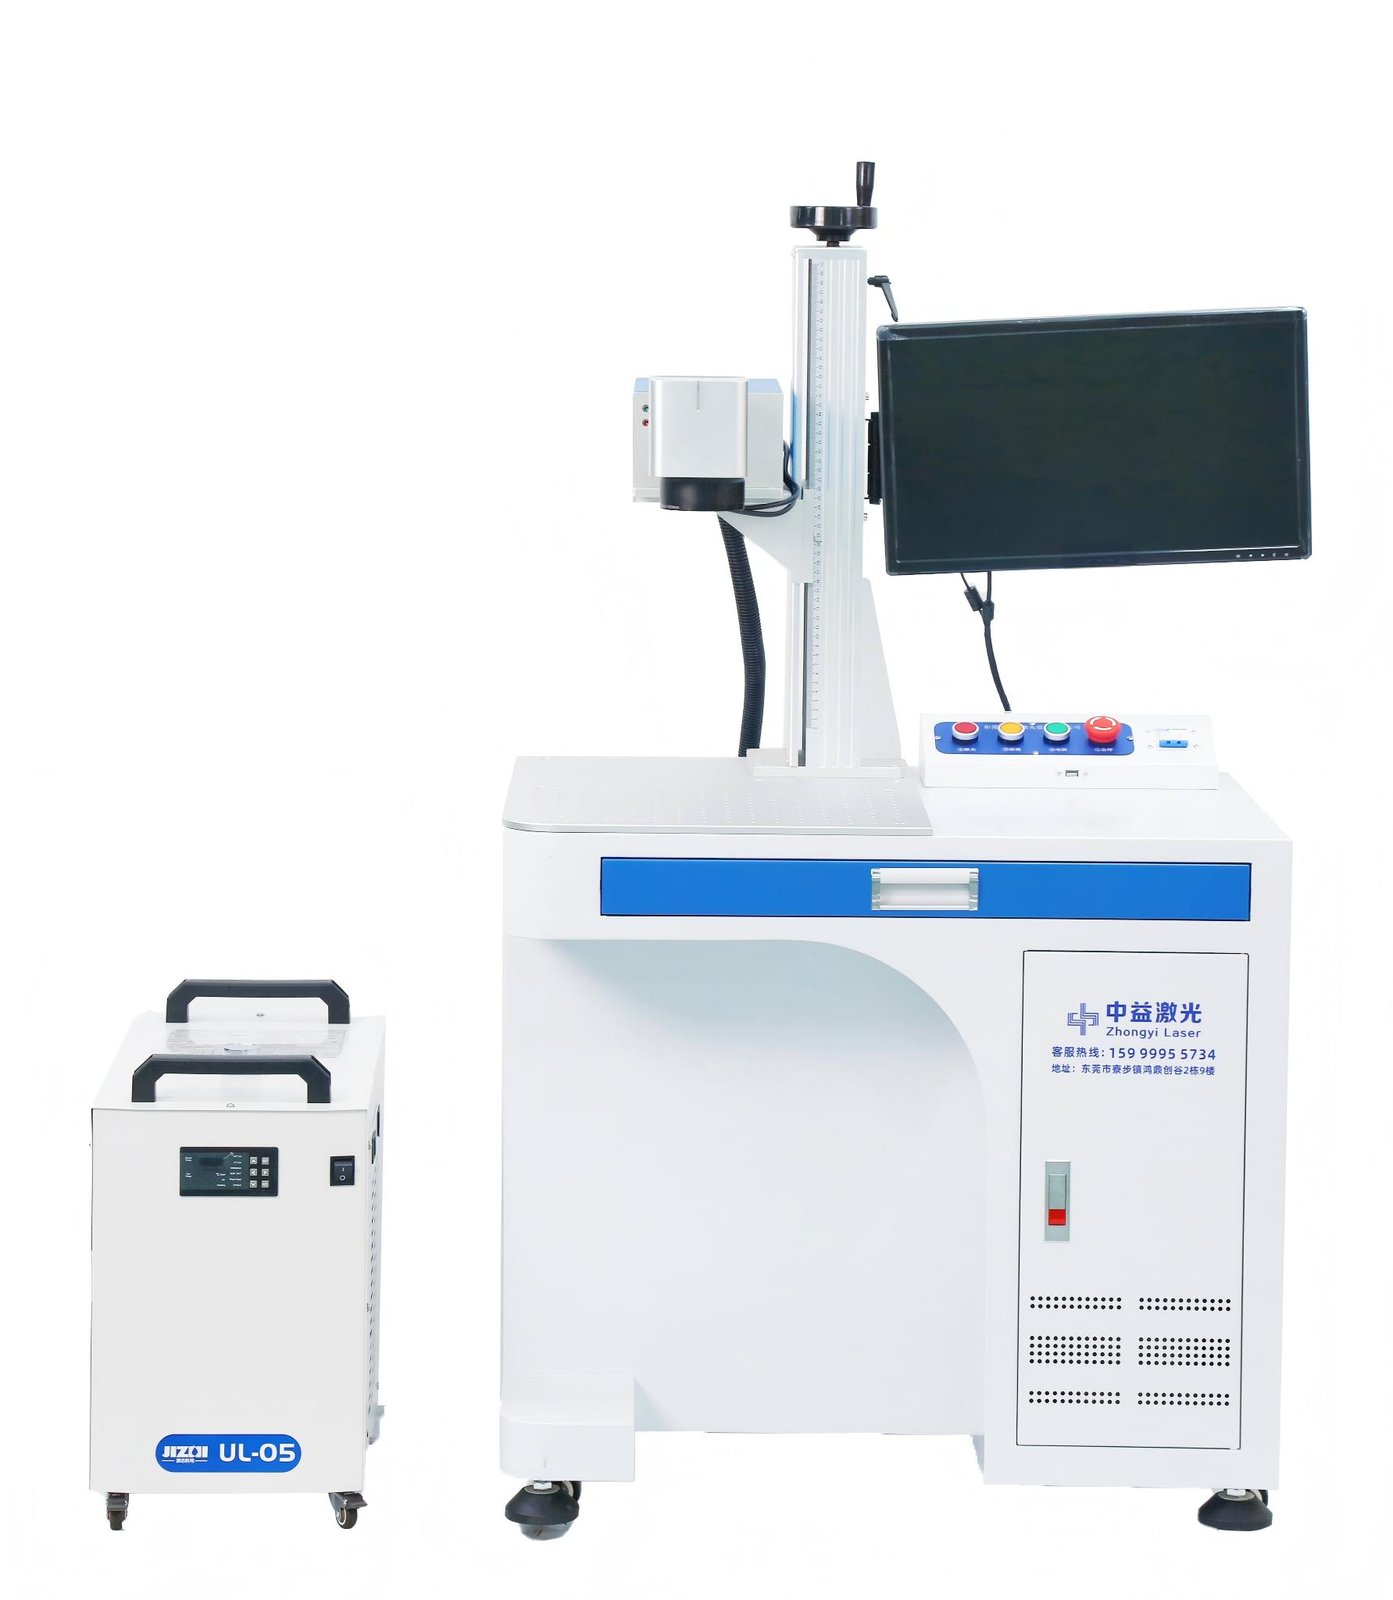
A UV laser marker works at 355 nm and is a cold process: photon energy breaks molecular bonds directly, stripping or modifying the surface photochemically with a minimal heat-affected zone, so heat-sensitive parts do not yellow, melt at the edges or stress-crack. Our UV platform focuses to 15 micrometres with plus or minus 0.02 mm repeatability, 110, 175 and 300 mm square fields, and a constant-temperature chiller locking the source temperature.
The answer and the process detail
The mark itself can satisfy UDI requirements for permanence and legibility - UV marks do not rub off and survive routine sterilisation. Compliance is a system question though: the coding rules, data structure and which database you submit to, such as GUDID in the US or EUDAMED in the EU, are set by the regulations of your market. The machine's job is to place a clean, durable code. We supply consistent marking quality and verifiable samples; the compliance sign-off sits with your regulatory team.
How to set it up and verify it
Three knobs set the process: power, repetition rate and scan speed, which together determine energy density per unit area. Start low and map a parameter window - sweep power and frequency at a fixed speed, find the cell where contrast is acceptable and the edge is not carbonised, then lock it into a process file with permissions. Remember that cold does not mean heat-free: too much power, too low a frequency or too many passes still accumulate heat, and thin stock will still perforate or curl.
Selection and delivery
3 W and 5 W suit thin materials and very shallow marking, 10 and 15 W suit large filled areas and poorly absorbing materials, and 20 W is built to order. The deciding factor is not precision, which is essentially identical at the same spot size, but cycle time: divide daily output by available hours and work back to the power you need. Still unsure, send samples - we mark them free at our Dongguan factory and return both the parts and a marking video within 24 hours. Full specifications, materials and buyer Q&A are on the UV Laser Marking Machine page.
Procurement Q&A
We have 3+ engineers, 7+ authorised patents and 5000+ units shipped. Standard parts like laser source and galvo are stocked long-term for predictable replenishment.
Price depends on the model (UV / fiber / CO₂), power, laser-source brand (Raycus / JPT / IPG) and configuration (galvo, field lens, control software). Zhongyi Laser lists the exact laser-source and galvo models on the quote and in the contract, so the configuration is verifiable and easy to reorder or replace later.
Standard machines ship in 7 days; rush orders in 3–5 days; custom non-standard builds in 15–30 days. Before production we confirm drawings, process and sample results to avoid rework.
18-month warranty on the machine. Core parts like the laser source and galvo are replaceable standard parts with long-term supply, so repairs and swaps are documented.
Yes. Send a sample and we return a real test video within 24 hours and ship the part back. Key models get a 48-hour aging test, so you see the actual result on your own workpiece before deciding.
Open Mo–Su 08:00–23:00 (GMT+8) with English support. Reach us at +86 159 9995 5734, WhatsApp +86 190 9874 6815 or Laurie@laserdg.com. Machines are packed to export standards.
The mark itself can satisfy UDI requirements for permanence and legibility - UV marks do not rub off and survive routine sterilisation. Compliance is a system question though: the coding rules, data structure and which database you submit to, such as GUDID in the US or EUDAMED in the EU, are set by the regulations of your market. The machine's job is to place a clean, durable code. We supply consistent marking quality and verifiable samples; the compliance sign-off sits with your regulatory team.
Not difficult, but it needs a method. The control software is JCZ EzCad with a straightforward interface; once a parameter file exists for a material, daily work is just recalling it. We supply manuals in Chinese and English plus video tutorials, and guide installation and first-piece setup remotely. The real hurdle is deciding what counts as acceptable - agree an internal standard using our sample parts first, then anyone can inspect against it.
They will not peel - UV modifies the surface rather than coating it, so bending cannot delaminate it. Two caveats: marking too deep weakens the substrate and the board may crack at the mark when flexed, and coverlay and solder mask absorb very differently, so parameters must be set for the actual layer. Keep to the minimum legible depth and run a flex-life test on the marked area.