Why this question comes up: the physics
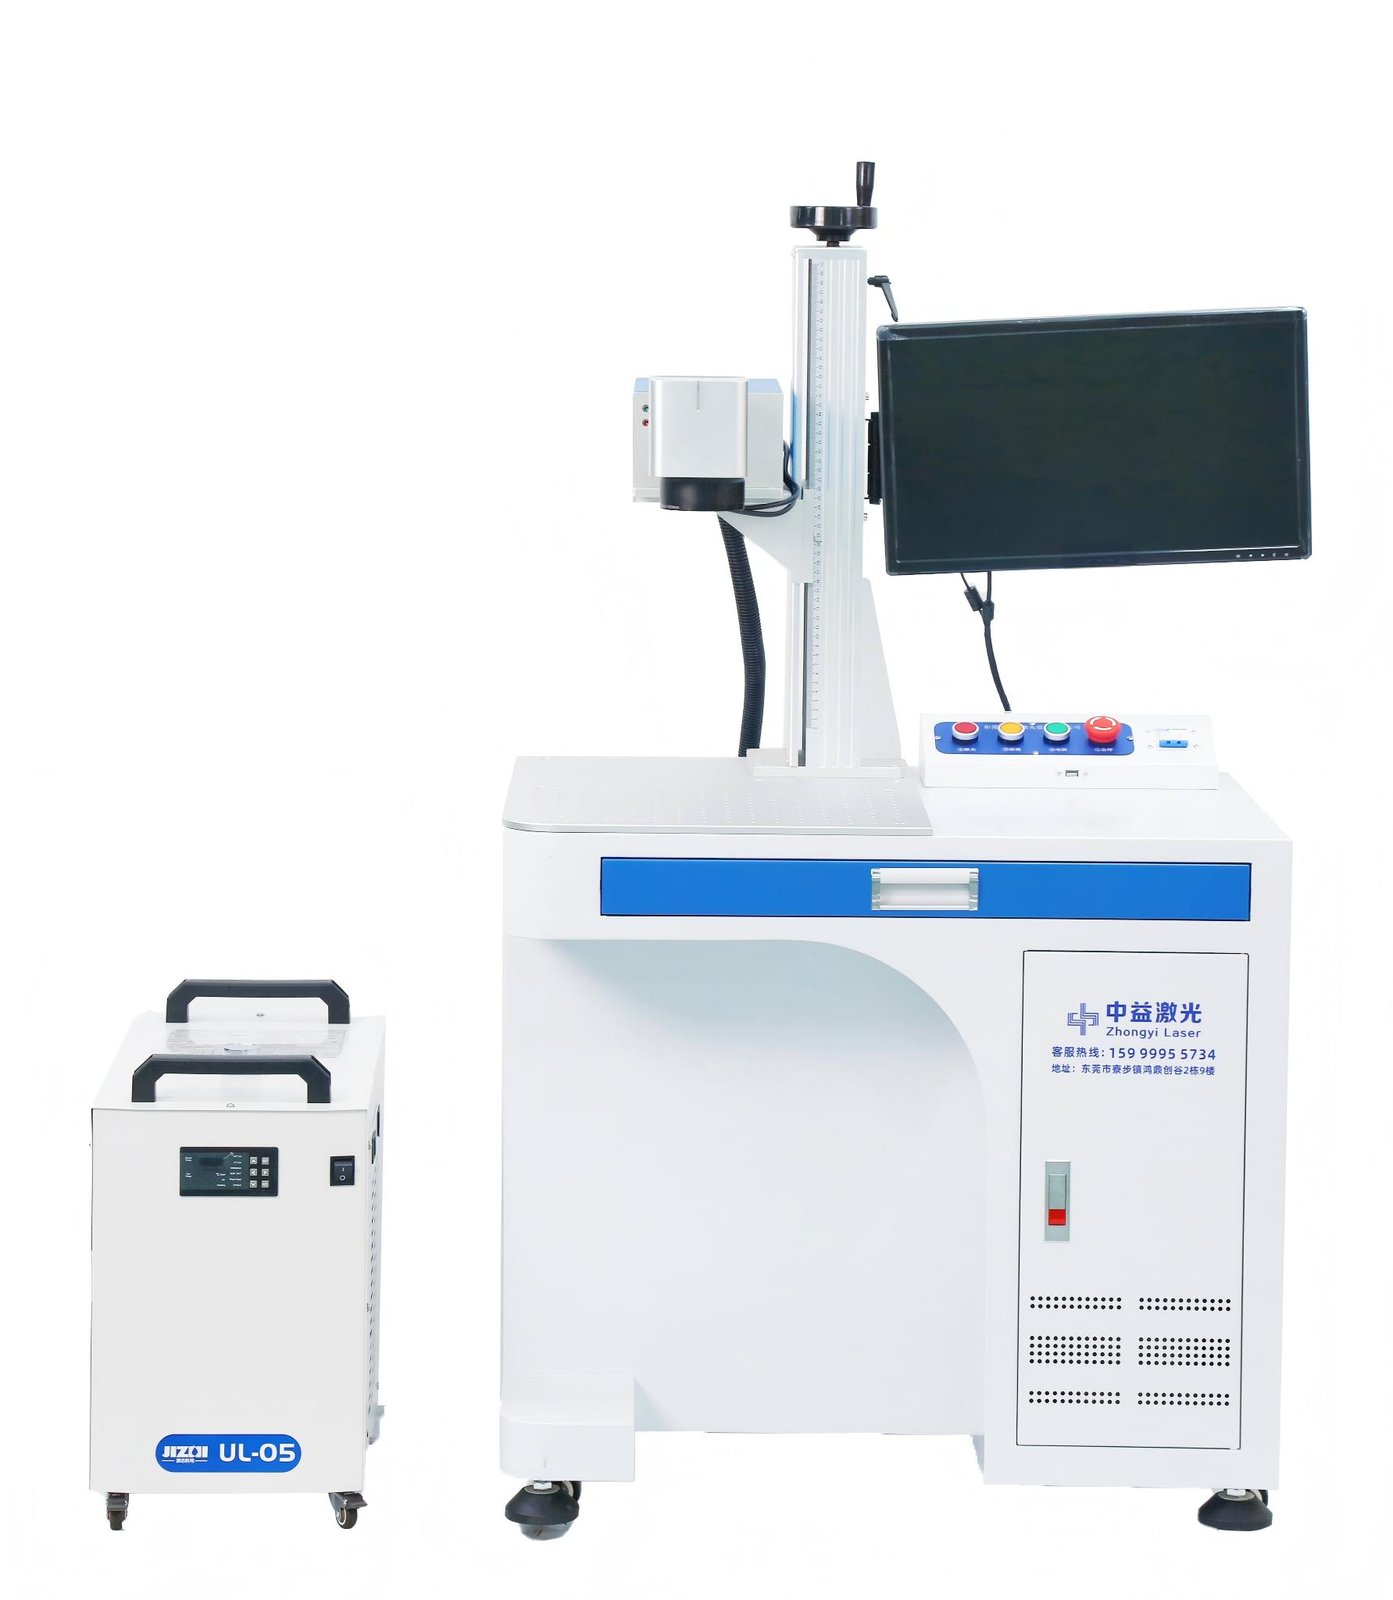
A UV laser marker works at 355 nm and is a cold process: photon energy breaks molecular bonds directly, stripping or modifying the surface photochemically with a minimal heat-affected zone, so heat-sensitive parts do not yellow, melt at the edges or stress-crack. Our UV platform focuses to 15 micrometres with plus or minus 0.02 mm repeatability, 110, 175 and 300 mm square fields, and a constant-temperature chiller locking the source temperature.
The answer and the process detail
UV modifies the surface layer itself rather than depositing a coating, so normal abrasion does not remove it. Durability is ultimately bounded by the substrate: anodised aluminium is hardest and most wear resistant, while painted or printed coatings are limited by the coating's own hardness. Where you need a number, run your own wear test - rubber or alcohol rub cycles - on the sample we mark and return to you.
How to set it up and verify it
Three knobs set the process: power, repetition rate and scan speed, which together determine energy density per unit area. Start low and map a parameter window - sweep power and frequency at a fixed speed, find the cell where contrast is acceptable and the edge is not carbonised, then lock it into a process file with permissions. Remember that cold does not mean heat-free: too much power, too low a frequency or too many passes still accumulate heat, and thin stock will still perforate or curl.
Selection and delivery
3 W and 5 W suit thin materials and very shallow marking, 10 and 15 W suit large filled areas and poorly absorbing materials, and 20 W is built to order. The deciding factor is not precision, which is essentially identical at the same spot size, but cycle time: divide daily output by available hours and work back to the power you need. Still unsure, send samples - we mark them free at our Dongguan factory and return both the parts and a marking video within 24 hours. Full specifications, materials and buyer Q&A are on the UV Laser Marking Machine page.
Procurement Q&A
We have 3+ engineers, 7+ authorised patents and 5000+ units shipped. Standard parts like laser source and galvo are stocked long-term for predictable replenishment.
Price depends on the model (UV / fiber / CO₂), power, laser-source brand (Raycus / JPT / IPG) and configuration (galvo, field lens, control software). Zhongyi Laser lists the exact laser-source and galvo models on the quote and in the contract, so the configuration is verifiable and easy to reorder or replace later.
Standard machines ship in 7 days; rush orders in 3–5 days; custom non-standard builds in 15–30 days. Before production we confirm drawings, process and sample results to avoid rework.
18-month warranty on the machine. Core parts like the laser source and galvo are replaceable standard parts with long-term supply, so repairs and swaps are documented.
Yes. Send a sample and we return a real test video within 24 hours and ship the part back. Key models get a 48-hour aging test, so you see the actual result on your own workpiece before deciding.
Open Mo–Su 08:00–23:00 (GMT+8) with English support. Reach us at +86 159 9995 5734, WhatsApp +86 190 9874 6815 or Laurie@laserdg.com. Machines are packed to export standards.
UV modifies the surface layer itself rather than depositing a coating, so normal abrasion does not remove it. Durability is ultimately bounded by the substrate: anodised aluminium is hardest and most wear resistant, while painted or printed coatings are limited by the coating's own hardness. Where you need a number, run your own wear test - rubber or alcohol rub cycles - on the sample we mark and return to you.
Stress cracking comes from localised heating and rapid cooling. Fiber at 1064 nm melts the material, which expands and builds internal stress at the interface, then cracks as it cools. UV at 355 nm breaks bonds photochemically: the energy is absorbed in a very thin surface layer with shallow heat diffusion, so bulk temperature rise and internal stress are far lower. The caveat is dose - excessive power still accumulates heat.
The control software is JCZ EzCad. It accepts image formats including bmp, jpg, gif, tga, png and tif, and vector formats including ai, dxf, dst and plt. Complex artwork can be designed in CorelDRAW, saved as plt and imported, then set up with line spacing and hatch parameters. Prefer vector - scaled bitmaps show jagged edges that hurt small character legibility.