Why maintenance decides mark quality
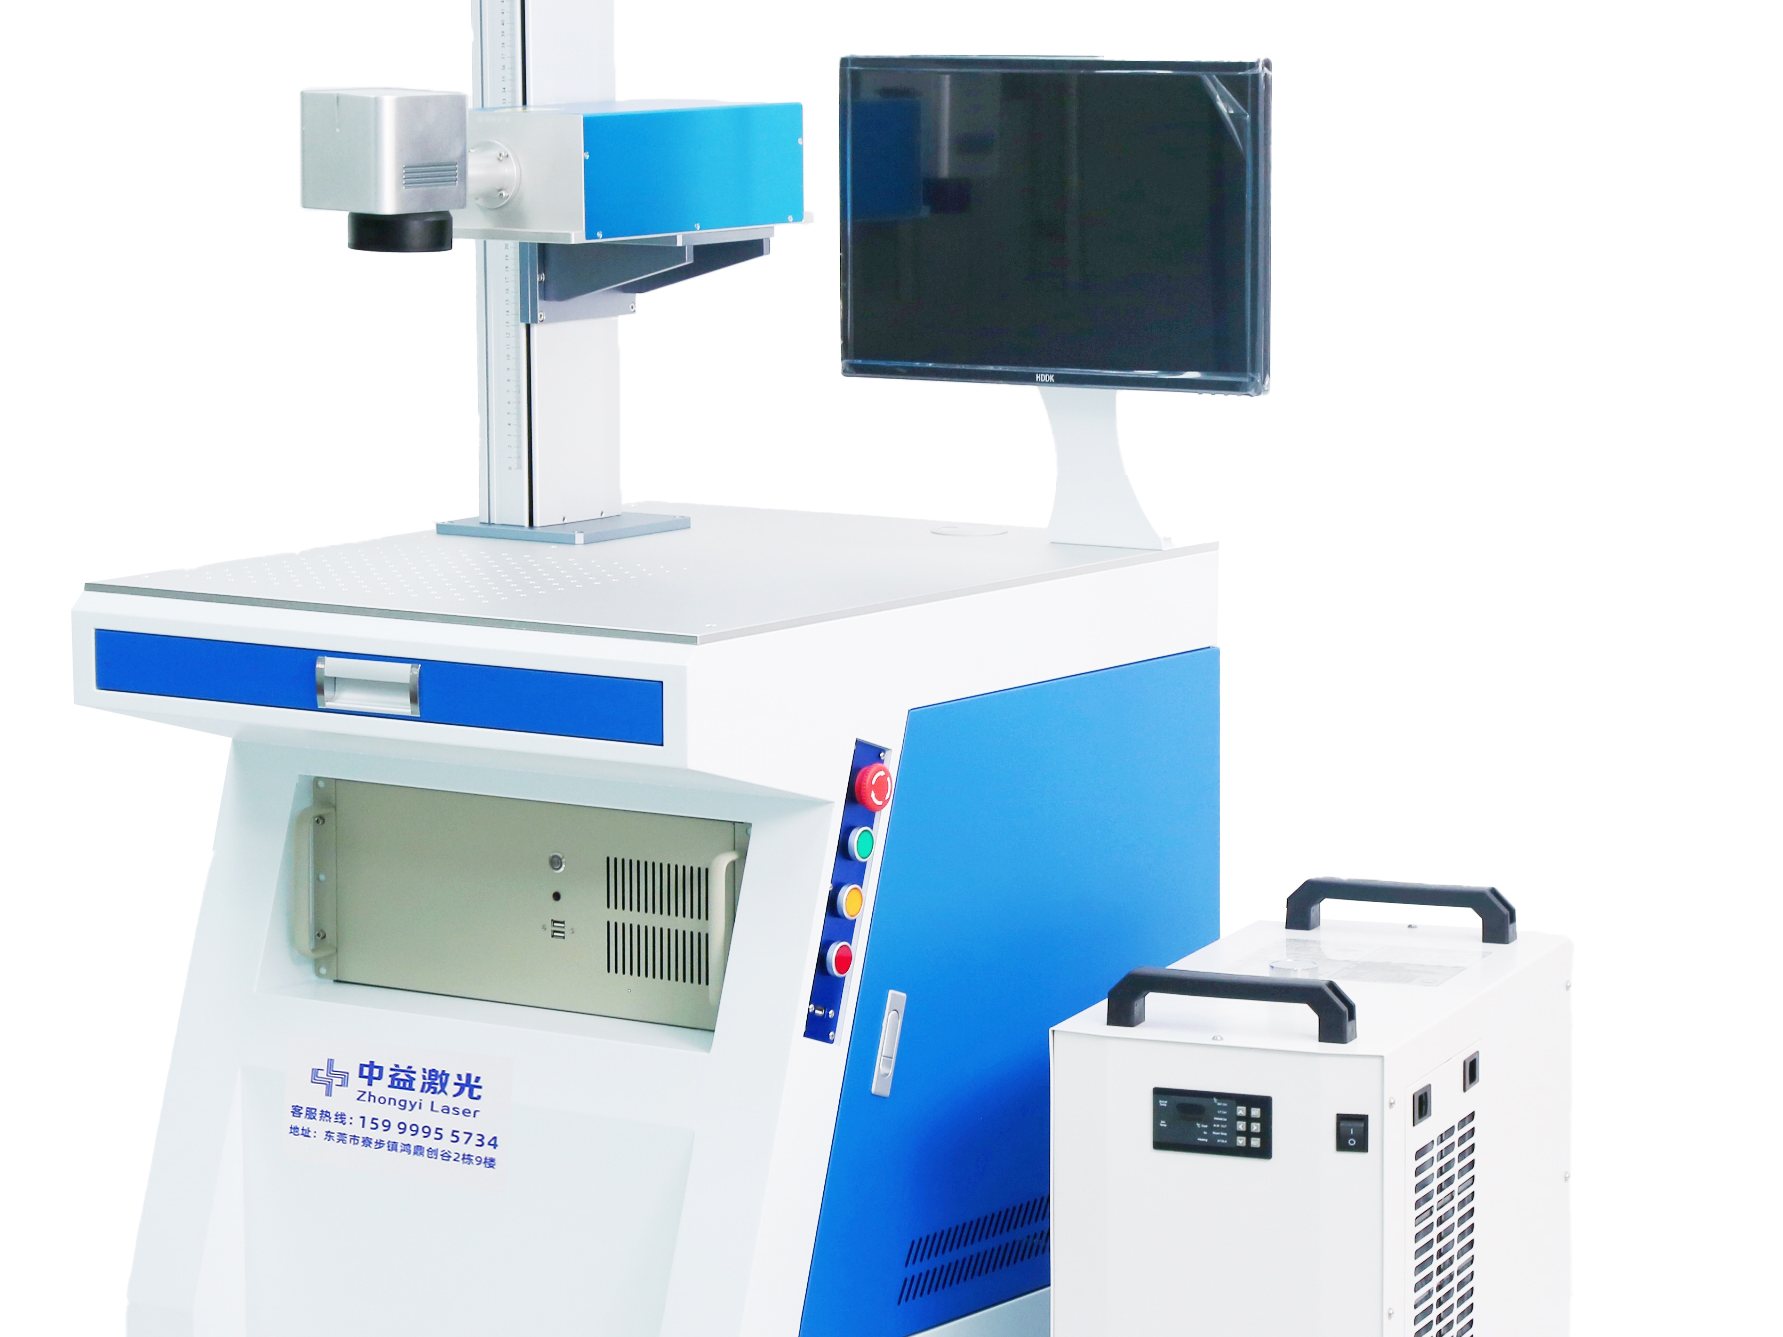
The beam leaves the source, passes through the protective window and the Field lens, and is focused onto the part. Dust or spatter on any of those surfaces attenuates the energy and scatters the spot. The symptoms are familiar: “it won’t go white anymore”, “it won’t go deep”, “the edges look fuzzy”. The first instinct is a failed laser source; more often it is a dirty lens.
The second common cause is cooling. High water temperature, dust-clogged air paths or a saturated filter make the source de-rate for protection. The symptom is a marking speed that quietly drops.
Daily · three minutes before start-up
- —Check chiller water temperature and level (water-cooled models), and listen for fan noise.
- —Inspect the Field lens and protective window for dust or spatter. Clean before starting, not after.
- —Clear debris from the worktable and fixture, and confirm the part locates the same way as yesterday.
- —Check air supply where used: stable pressure, clear nozzle.
- —Run one scrap test piece and compare the result with yesterday’s.
Weekly
- —Clean the protective window and Field lens with lens tissue or a lint-free wipe and anhydrous ethanol (or a dedicated lens cleaner). Wipe in one direction — never back and forth — and use each tissue once.
- —Verify focus, and that the red pointer and the actual mark coincide.
- —Clear dust from cabinet vents and fan filters.
- —Check coolant (water-cooled models) for cloudiness or yellowing; replace if needed.
Monthly
- —Clean the internal cooling path thoroughly — power down first.
- —Inspect cables and connectors for looseness or wear; confirm the earth connection.
- —Back up software parameters and marking files. Saving a tuned parameter set as a recipe costs far less than re-tuning.
- —Check the galvo and Field lens mounting screws. Looseness shows up directly as position drift.
- —Log this month’s issues and fixes — your own machine history.
Wear parts and intervals
| Part | Typical interval | Note |
|---|---|---|
| Protective window | Replace when soiled or scratched | Inexpensive consumable — do not stretch it; scratches propagate to the Field lens |
| Field lens | Years, depending on duty | Once the coating is damaged, mark edges visibly soften |
| Coolant / filter | 3–6 months (water-cooled) | Poor water quality directly shortens source life |
| Fan filter mat | Clean at 1–3 months; replace if torn | Affects cabinet cooling and dust ingress |
| Air line filter | By pressure stability | Failed oil/water separation contaminates optics |
The four most common mistakes
- —Wiping a lens with a hand or household tissue: paper fibres and skin oil cause permanent scratches. Use lens tissue and anhydrous ethanol, one direction, light pressure.
- —Running at full power by default: mark as lightly as the job allows. Sustained full power accelerates source degradation.
- —Skimping on earthing: static and interference cause position errors and dropped points, and can damage the control board.
- —Ignoring a chiller alarm: pushing on through a temperature warning is one of the leading causes of premature source failure.
If something goes wrong
Do not open the machine yet. Send us a short video with three facts: the material, the parameters, and when the behaviour changed. Remote video troubleshooting resolves most issues far faster than shipping the unit back.
Zhongyi Laser dispatches spare parts as agreed, and overseas customers can book an engineer for remote debugging.
Keeping a machine factory-fresh
Maintenance is half of it; the original configuration is the other half. The laser source is selectable to your budget (Raycus / JPT / IPG), and the galvo and Field lens models are written into the contract. Same machine, different components — a very different two-year stability profile.